简体中文
 English
 Español
News
Commercial Food Display Warmer and Cake Showcase: A Practical Guide to the XCR-136L
In commercial food service, presentation and holding performance are closely connected. A product may look attractive when it first leaves the kitchen, but its value can decline quickly if it is exposed to unsuitable temperatures, poor lighting, condensation, or an unorganized display environment. A professional food display warmer addresses these challenges by combining controlled heating, visible presentation, accessible storage, and a design suited to demanding retail and hospitality settings.
The XCR-136L is a 136-liter food display warmer designed for cake showcases, prepared food counters, bakeries, cafés, restaurants, convenience stores, hotel breakfast areas, and other commercial environments. Its operating temperature range is 30°C to 90°C, allowing operators to select a suitable holding temperature for different warm food applications. With a rated input power of 1100 watts, a digital thermostat and display, internal LED illumination, automatic defrost, and a direct cooling system, the unit is designed to combine practical control with a clear product presentation.
This article examines the design, operating characteristics, commercial benefits, manufacturing strengths, and purchasing considerations associated with the XCR-136L. It also explains how a purpose-built display warmer can provide advantages over basic heated shelves, improvised counter displays, and less coordinated equipment used by competing suppliers.
1. The Role of a Professional Food Display Warmer
A food display warmer is more than a heated cabinet. It is a merchandising tool, a food-holding appliance, and a front-of-house equipment solution in one unit. The equipment must keep food warm while allowing customers to see the products clearly. It must also help staff replenish, organize, and monitor items during busy service periods.
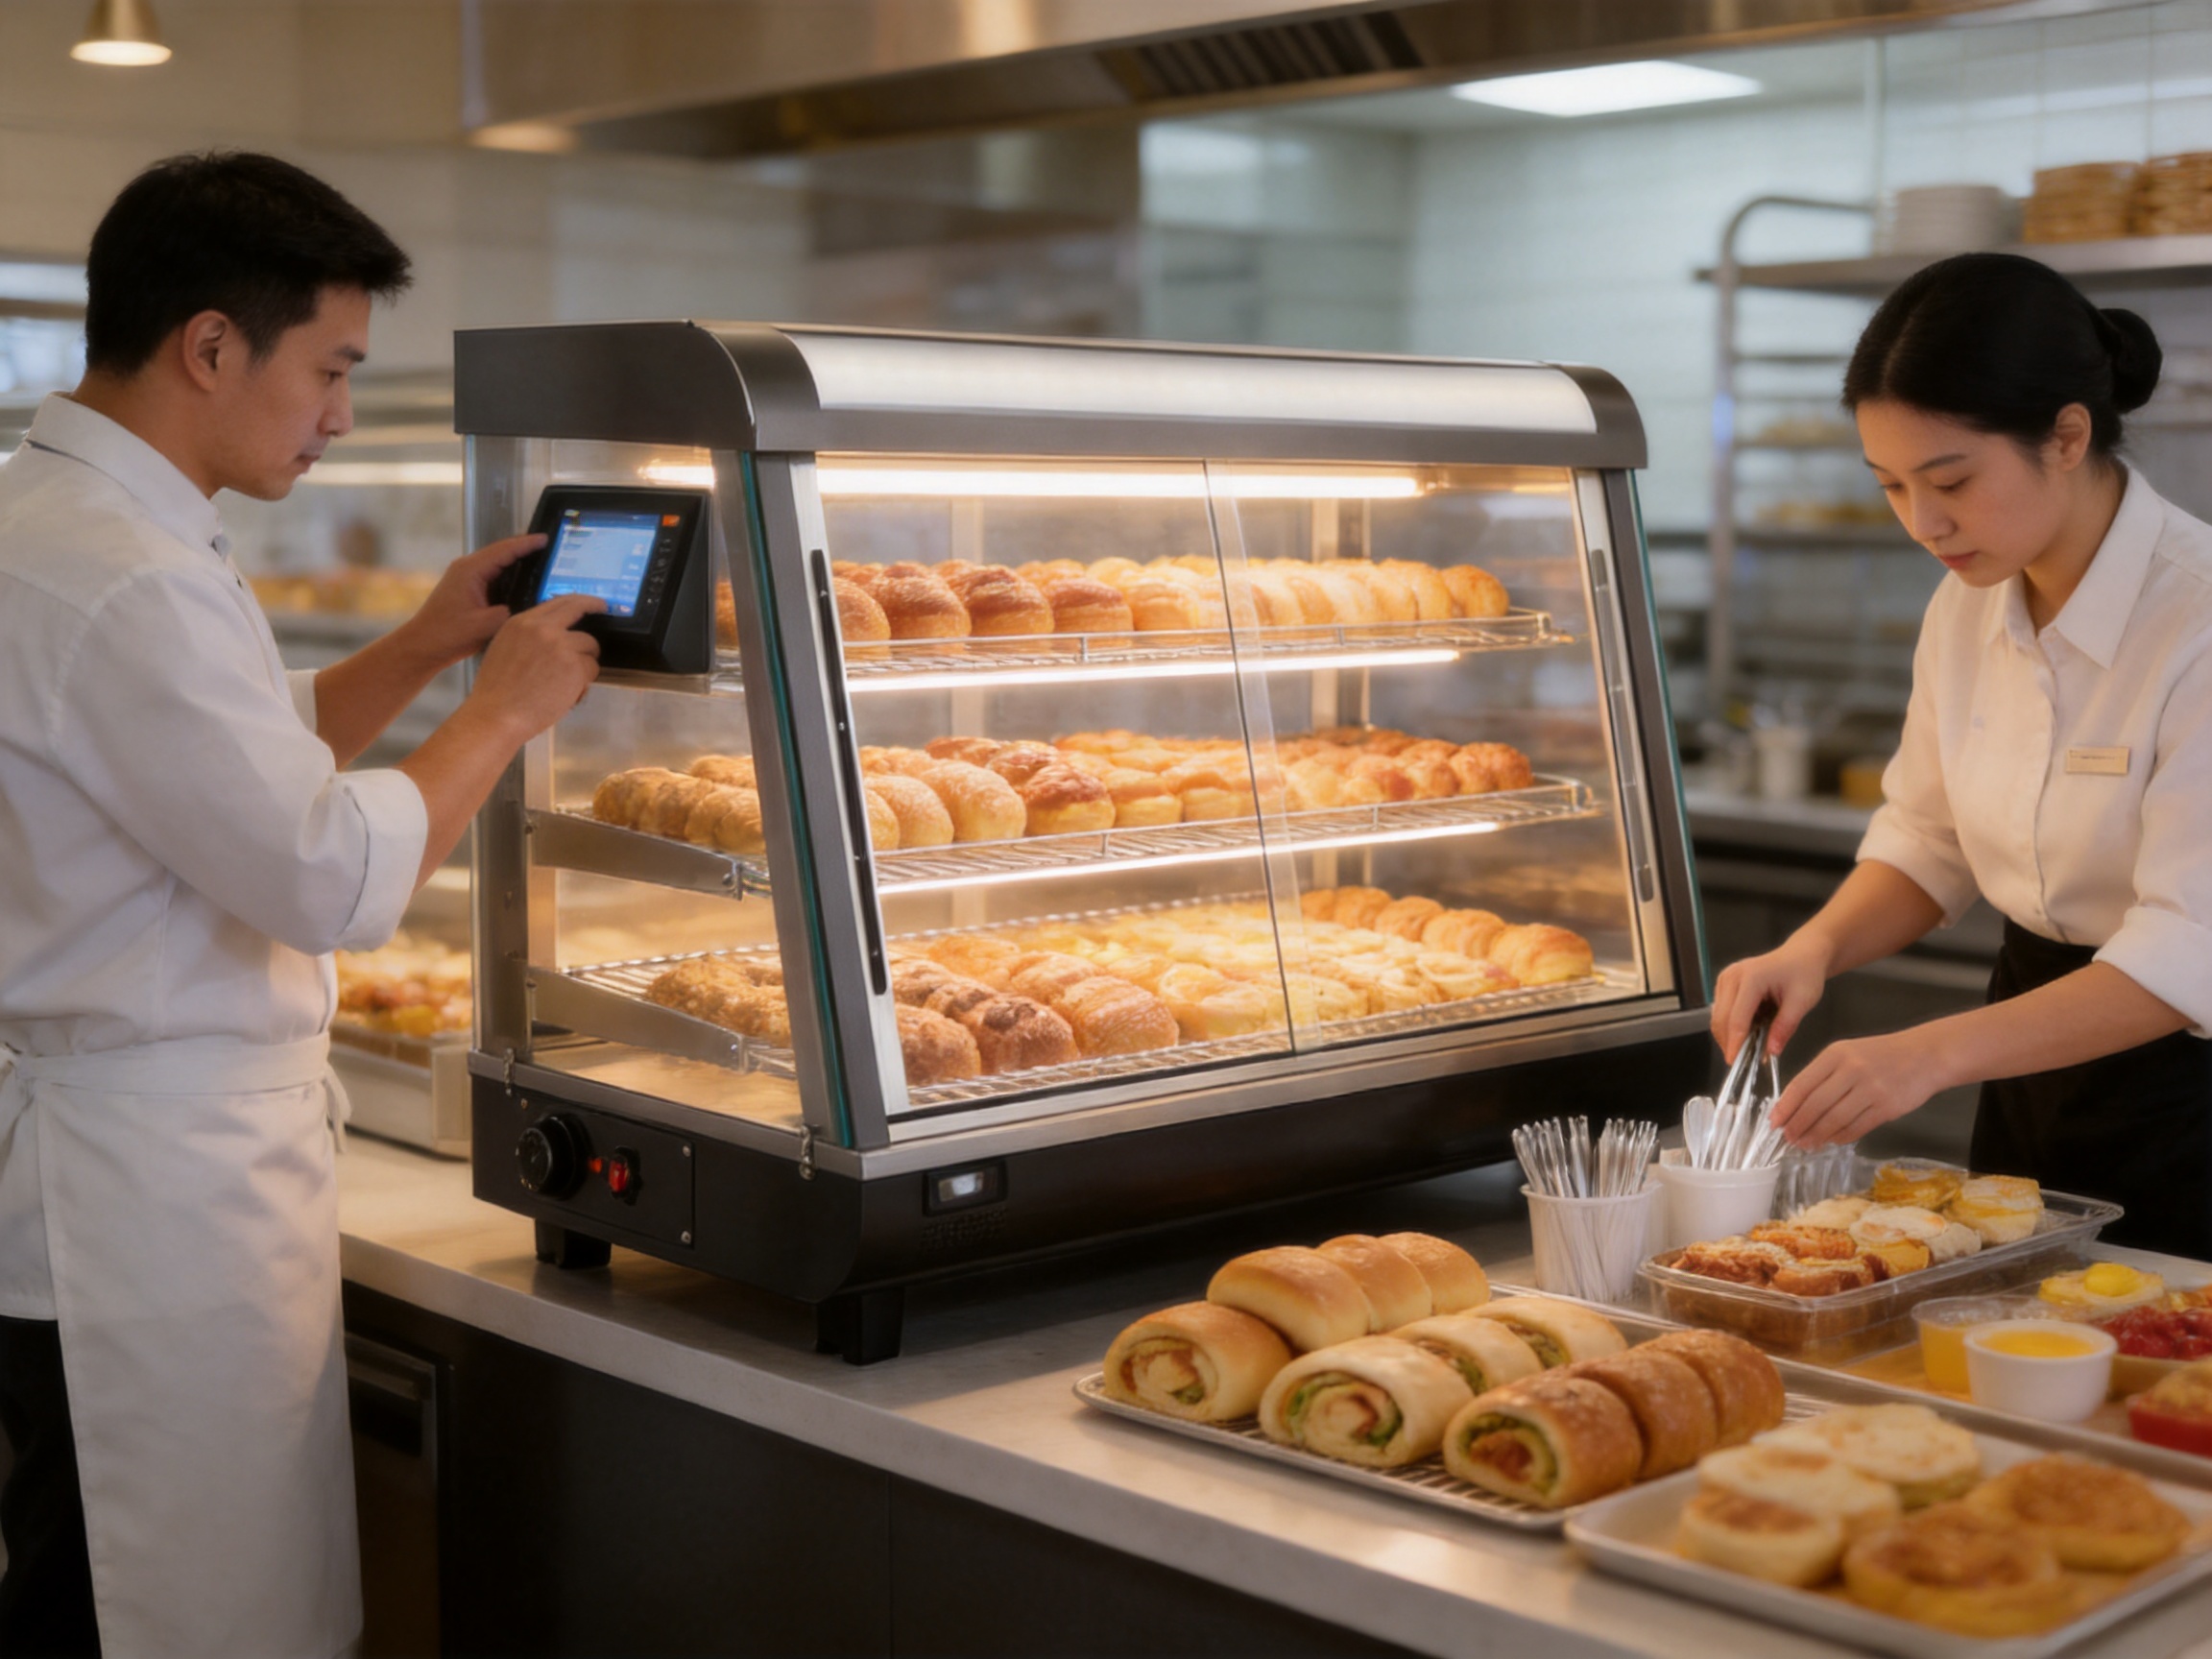
Many commercial foods are prepared in batches. Pastries, cooked snacks, roasted products, breakfast items, filled sandwiches, baked goods, and hot takeaway meals may all need to remain available for customers after preparation. If these products are left on an open counter, they can lose heat rapidly and may be exposed to dust, air movement, accidental contact, or inconsistent serving conditions. A display warmer provides a more controlled environment while preserving the visual appeal that encourages purchase.
Traditional open heated shelves may be useful for simple service lines, but they often provide limited protection and limited merchandising impact. A closed or glazed display format can make the product area look more organized and professional. It also helps separate displayed food from the surrounding retail environment. The XCR-136L is intended for businesses that want the practical performance of a warmer together with the visual advantages of a showcase.
Temperature control is especially important when products must be held for a period before sale. Excessive heat can dry food, alter texture, or reduce quality. Insufficient heat may fail to meet the operator’s holding objectives. A variable range from 30°C to 90°C gives the user greater control than equipment operating at only one fixed temperature. The correct setting will depend on the food type, local food-safety procedures, product turnover, and the operator’s own operating instructions.
2. Product Overview
The XCR-136L has a rated capacity of 136 liters. This capacity is suitable for compact commercial operations and for larger premises that require an additional service station. It can serve as a primary display warmer in a small bakery or café, or as a supplementary unit in a busy restaurant, hotel, food court, or convenience store.
The product is classified as a display warmer and food display showcase. Its design is intended to place warm products in a visible front-of-house position. The external dimensions are 904 millimeters in length, 486 millimeters in width, and 636 millimeters in height. This footprint provides a useful balance between display volume and counter efficiency.
At less than one meter in length, the unit can fit on many commercial counters without consuming the space required by a full-size floor-standing cabinet. Its depth of 486 millimeters is also suitable for installations where counter depth is limited. Operators should still check ventilation, access, electrical clearance, service space, and the dimensions of the intended installation area before ordering.
The net weight is 38 kilograms, while the gross shipping weight is 41 kilograms. The difference reflects packaging materials and shipping protection. The package dimensions are 963 by 549 by 675 millimeters, which should be considered when planning delivery routes, loading access, door clearance, storage, and installation.
Product Attribute | Specification |
Model | XCR-136L |
Product type | Commercial food display warmer |
Primary applications | Cake showcase, bakery display, prepared food display, café and restaurant service |
Capacity | 136 liters |
Temperature range | 30°C to 90°C |
Input power | 1100 watts |
Net weight | 38 kilograms |
Gross weight | 41 kilograms |
Product dimensions | 904 × 486 × 636 millimeters |
Package dimensions | 963 × 549 × 675 millimeters |
20-foot general-purpose container quantity | 72 units |
40-foot high-cube container quantity | 192 units |
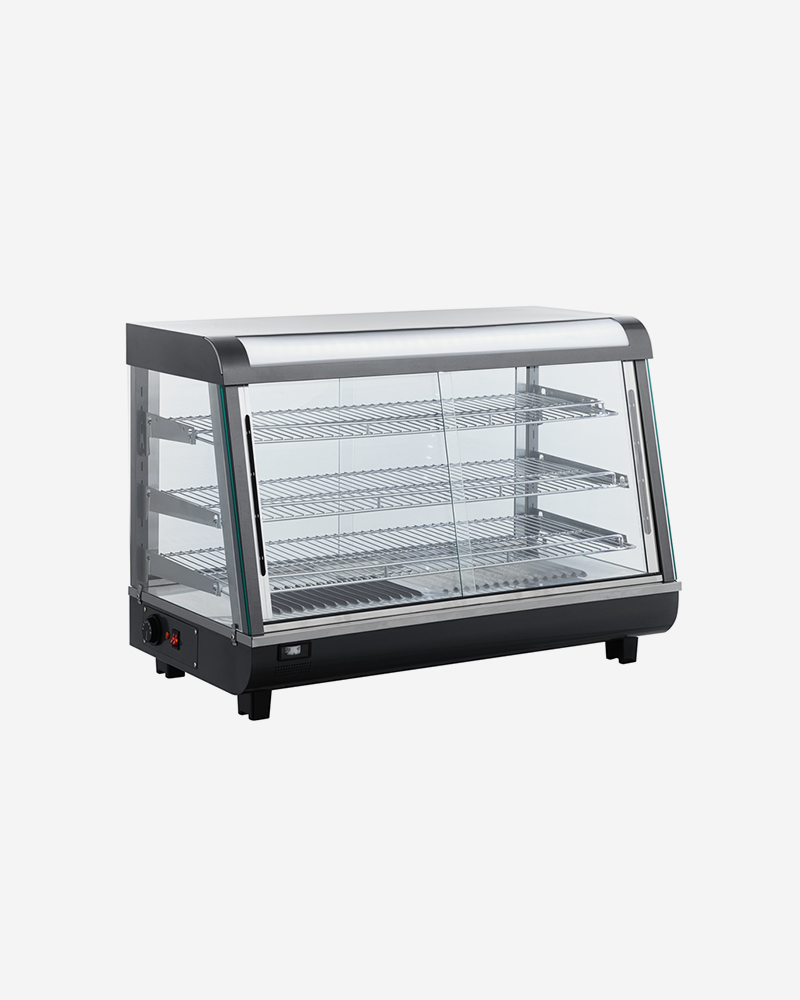
Display Equipment Food Display Warmer Cake Showcase
3. Temperature Control for More Consistent Holding
The temperature range is one of the most important features of the XCR-136L. The unit can be adjusted from 30°C to 90°C, giving operators the ability to select a holding condition suited to the product and service plan. Lower settings may be useful for products that require gentle warming, while higher settings may be used for products that need a stronger heat-holding environment.
The appropriate temperature should never be selected solely by appearance. Operators should consider the product composition, moisture content, serving duration, local regulations, internal food-safety procedures, and guidance from the food producer. The display warmer helps provide an adjustable operating platform, but staff training and regular monitoring remain essential parts of safe commercial food handling.
The digital thermostat and display make the set point easier to read and manage than a basic mechanical dial. A digital control interface can help staff identify the selected temperature quickly during opening checks, replenishment, and closing procedures. It can also support more consistent operation when multiple employees use the same cabinet.
Consistency is valuable for both product quality and business management. If one shift uses a high setting and another uses a low setting, customers may receive noticeably different products. A visible digital display reduces ambiguity and gives employees a clearer reference. It also helps supervisors identify whether the equipment is operating at the intended setting.
Temperature control is particularly useful when the display contains multiple food categories. A bakery may use the showcase for heated pastries, savory baked items, and prepared snacks. Although these products may not require identical treatment, an adjustable cabinet gives the operator more flexibility than a permanently fixed warmer.
4. Evaporator Arrangement and Internal Environment
The standard features include both top and bottom evaporators. This arrangement is designed to support temperature distribution through the display area. A top-and-bottom configuration can help the cabinet address temperature variation between upper and lower sections, although actual performance will depend on loading, ambient conditions, product placement, door or access frequency, and installation conditions.
The presence of both upper and lower evaporator components is an important distinction when comparing equipment. Some basic display warmers rely on a single heating source or a simple exposed element. Such designs may provide less coordinated control throughout the cabinet. A dual-position arrangement gives the manufacturer a more structured approach to managing the internal environment.
The water channel under the top evaporator is another practical feature. In commercial display equipment, condensation and moisture management can affect visibility, cleanliness, and maintenance. A designated water channel provides a planned route for water management beneath the top evaporator instead of leaving moisture to collect unpredictably in the cabinet.
Moisture control is especially relevant in environments where the display is opened frequently or where warm food releases humidity. Without a suitable drainage or collection arrangement, condensation can affect the appearance of glass and internal surfaces. Staff should still clean the water channel regularly and follow the recommended maintenance procedure to prevent residue or blockage.
The direct cooling system contributes to the operating design specified for the unit. Direct systems are commonly used in commercial equipment because they provide a straightforward method of transferring thermal energy within the cabinet. Their performance depends on correct loading, proper installation, regular cleaning, and adherence to the operating instructions.
5. Automatic Defrost and Service Convenience
Automatic defrost is included among the standard features. Defrost management is important because moisture can accumulate during operation, especially when the cabinet is used frequently or exposed to changing ambient conditions. If frost or excessive moisture is allowed to build up, it may affect thermal performance, visibility, cleanliness, and component life.
Automatic defrost reduces the need for staff to interrupt service for frequent manual defrost cycles. This can be valuable in a retail environment where the display is expected to remain available throughout the business day. It also supports more predictable routine operation and can simplify maintenance planning.
Automatic defrost does not eliminate the need for cleaning and inspection. Staff should still examine internal surfaces, water channels, glass panels, seals, shelves, and accessible components. Food residue should be removed according to the manufacturer’s care instructions. Maintenance is most effective when it is scheduled rather than performed only after a visible problem develops.
For purchasing managers, the combination of automatic defrost and a digital control system can reduce operational complexity. Equipment that is easier to understand and maintain generally places fewer demands on staff training. This is particularly useful for multi-site operators, franchise groups, and businesses with rotating employees.
6. Internal LED Lighting and Product Merchandising
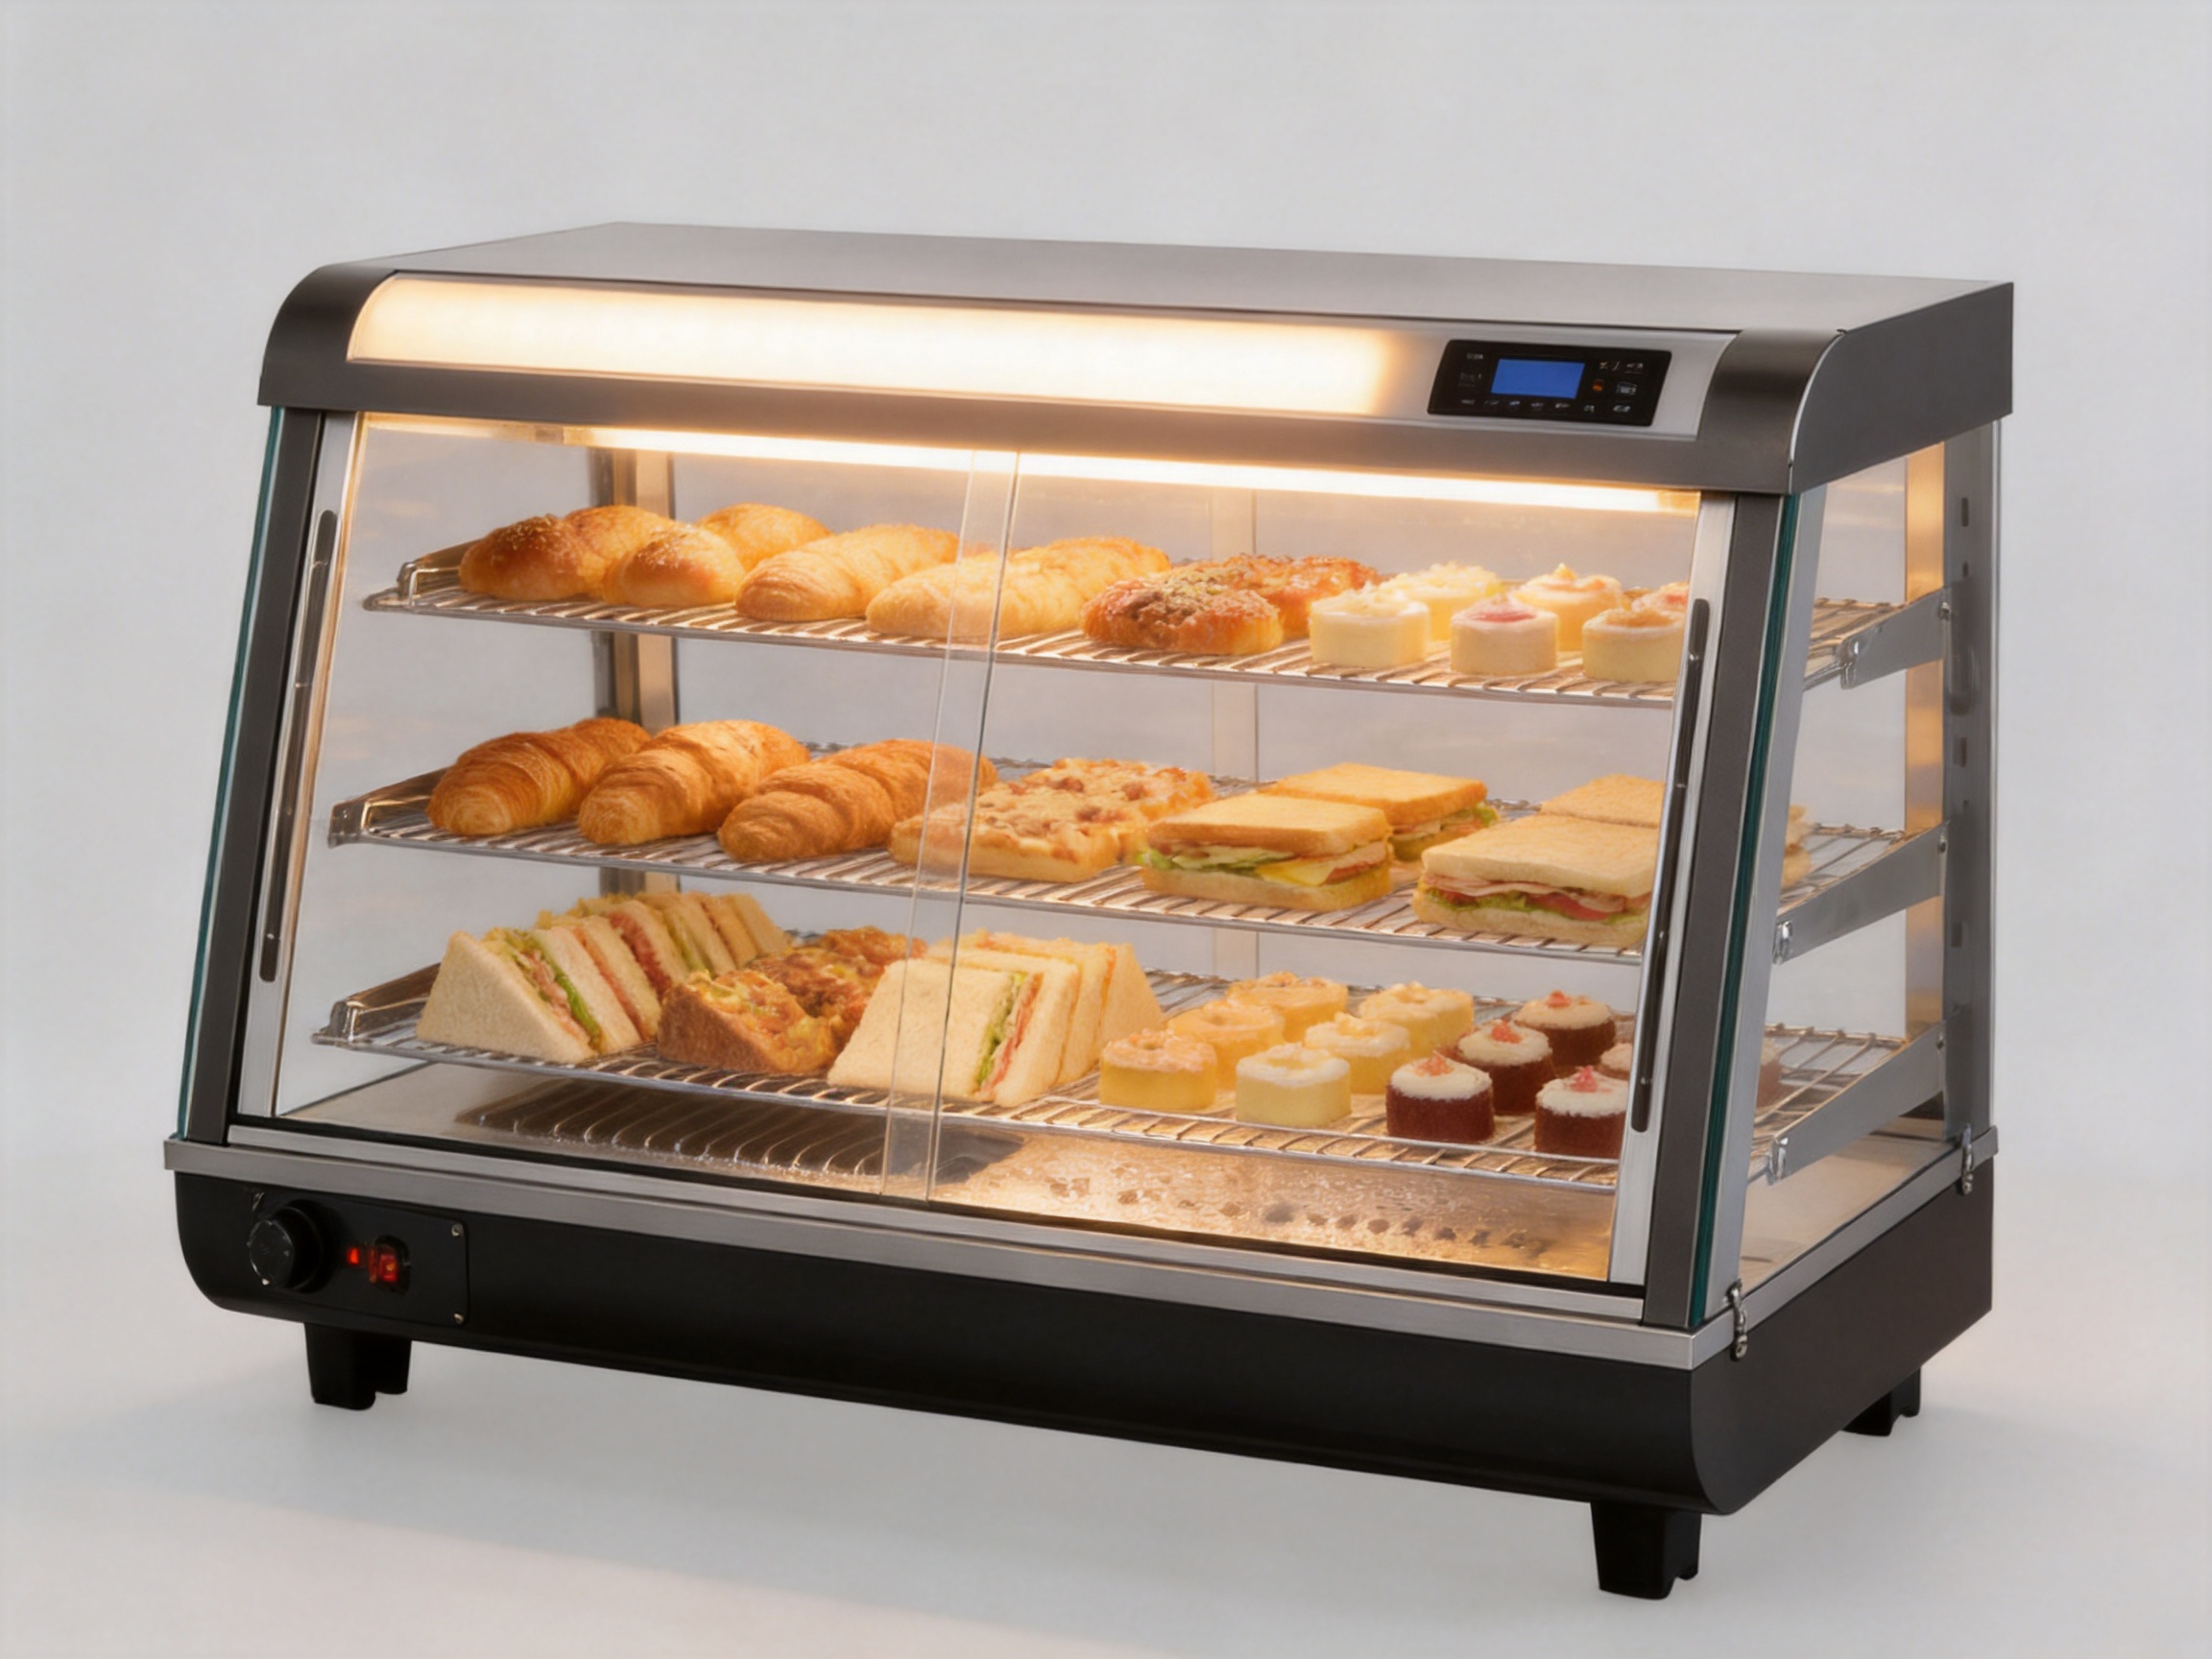
Lighting has a direct influence on how customers perceive displayed food. The XCR-136L includes an internal top LED light to illuminate the presentation area. A well-lit display can help customers identify product shapes, colors, toppings, fillings, and packaging details without opening the cabinet or asking a member of staff to explain every item.
The top-mounted internal position helps direct attention toward the displayed products. LED lighting is widely used in modern commercial equipment because it can provide bright illumination with relatively low heat output compared with older lighting technologies. Lower heat contribution is useful in a temperature-controlled food display because lighting should support visibility without unnecessarily affecting the internal environment.
Good lighting also supports merchandising discipline. When products are clearly visible, staff are more likely to notice empty spaces, uneven placement, or items requiring replenishment. This makes the display easier to manage during service. A tidy, consistently illuminated showcase can contribute to a stronger perception of freshness and professionalism.
For cake and bakery applications, lighting is particularly important. Decorative details can be lost in a dim cabinet, while excessive glare can make products difficult to view. Operators should position the display to minimize reflection from overhead lighting and windows. The final visual result depends on both the built-in LED and the surrounding store environment.
7. Advantages in Comparison with Basic Competitor Equipment
Every commercial equipment comparison should consider the full operating requirement rather than focusing on a single specification. The XCR-136L offers several practical advantages when compared with basic warming shelves, manually controlled cabinets, and less organized display solutions.
7.1 Adjustable operating range
A fixed-temperature warmer may be adequate for one product category, but it can be limiting when a business sells a varied menu. The XCR-136L provides a 30°C to 90°C range, allowing the operator to adapt the cabinet to different warm display requirements. This flexibility can make the equipment more useful as the product range changes over time.
7.2 Digital thermostat and display
Digital control provides a clear reference for employees and managers. Compared with a basic dial, the digital display can make the selected temperature easier to identify and reproduce. It also supports more consistent shift-to-shift operation, provided staff follow the same procedures.
7.3 Planned moisture management
The water channel under the top evaporator shows that moisture handling has been considered in the cabinet design. This can offer a practical advantage over improvised equipment where condensation collects on uncontrolled surfaces. A planned channel is easier to inspect and include in a regular cleaning routine.
7.4 Dual evaporator arrangement
The top and bottom evaporator configuration is intended to support the internal operating environment across the display area. It provides a more coordinated design than a single basic heating point and may assist with more balanced cabinet performance when the unit is loaded correctly.
7.5 Automatic defrost
Automatic defrost can reduce service interruptions and manual maintenance work. It is a useful feature for businesses that need a display warmer to operate throughout long opening hours. The reduced need for manual intervention can also help standardize daily routines.
7.6 Compact commercial footprint
The dimensions of 904 by 486 by 636 millimeters make the unit suitable for counter installation where space is valuable. Some competing cabinets may offer greater capacity but require a much larger footprint. Others may be compact but provide inadequate display volume. The XCR-136L occupies a middle position for operators seeking usable capacity without immediately committing to a large floor-standing cabinet.
7.7 Combined display and warming function
Businesses can sometimes reduce counter clutter by using one purpose-built display warmer instead of combining a separate heated tray, a light box, and an open merchandising rack. Consolidating functions may create a cleaner service area and simplify the customer’s visual experience.
These advantages should be evaluated together with price, local electrical requirements, warranty terms, service availability, shipping conditions, and the operator’s food-handling procedures. No single cabinet is ideal for every menu or premises. The strength of the XCR-136L is its combination of adjustable warming, visible presentation, moisture management, and compact commercial design.
8. Applications Across Commercial Food Service
8.1 Bakeries and pastry shops
Bakeries can use the XCR-136L to present warm pastries, savory baked goods, filled rolls, breakfast items, and selected specialty products. The illuminated display helps customers see the range before making a purchase. A counter-height installation can also place products close to the point of sale, encouraging impulse purchases and simplifying staff access.
The cabinet can be used alongside a separate refrigerated cake showcase when a business sells both chilled desserts and warm bakery products. This division allows each product category to receive more suitable treatment instead of placing all items in one general-purpose display.
8.2 Cafés and coffee shops
Cafés often need a compact cabinet that supports breakfast service, lunch snacks, and afternoon food sales. The XCR-136L can be positioned near the coffee counter or collection point to display warm items without taking up the space required for a full commercial kitchen appliance.
For cafés, the display effect is as important as the holding function. Customers can make decisions while waiting for beverages, and staff can identify which products require replenishment. The cabinet can therefore support both service efficiency and additional sales opportunities.
8.3 Restaurants and hotel breakfast areas
Restaurants may use the unit for appetizers, baked side dishes, hot snacks, or service-line items. Hotels can position it in a breakfast area or event service station. Its moderate capacity allows operators to create a focused display rather than overfilling a large cabinet with products that may lose quality before sale.
In buffet applications, staff should manage replenishment carefully. Smaller batches placed at regular intervals may maintain better appearance and quality than one heavily loaded display. The warmer can support this approach by providing a visible, controlled location for ready-to-serve products.
8.4 Convenience stores and takeaway outlets
Convenience stores and takeaway businesses often depend on quick purchase decisions. A well-lit warmer placed near the checkout area can present hot snacks and prepared foods where customer traffic is highest. The compact form can make it easier to install the cabinet in an existing retail layout.
Because these businesses may operate for extended hours, automatic defrost and digital temperature control can be particularly useful. Employees can incorporate basic temperature checks, cleaning, replenishment, and visual inspection into standard opening and closing procedures.
8.5 Catering and institutional service
Catering businesses, school cafeterias, workplace dining areas, and institutional kitchens may use the equipment for short-term display before scheduled service. The cabinet’s adjustable range gives operators flexibility for different menu cycles, while the illuminated front presentation can help identify menu choices quickly.
Institutional users should confirm that the cabinet’s dimensions, electrical configuration, capacity, and cleaning requirements align with their purchasing standards. They should also ensure that local regulations and internal hygiene procedures are observed.
9. Manufacturing Strength and Product Development Capability
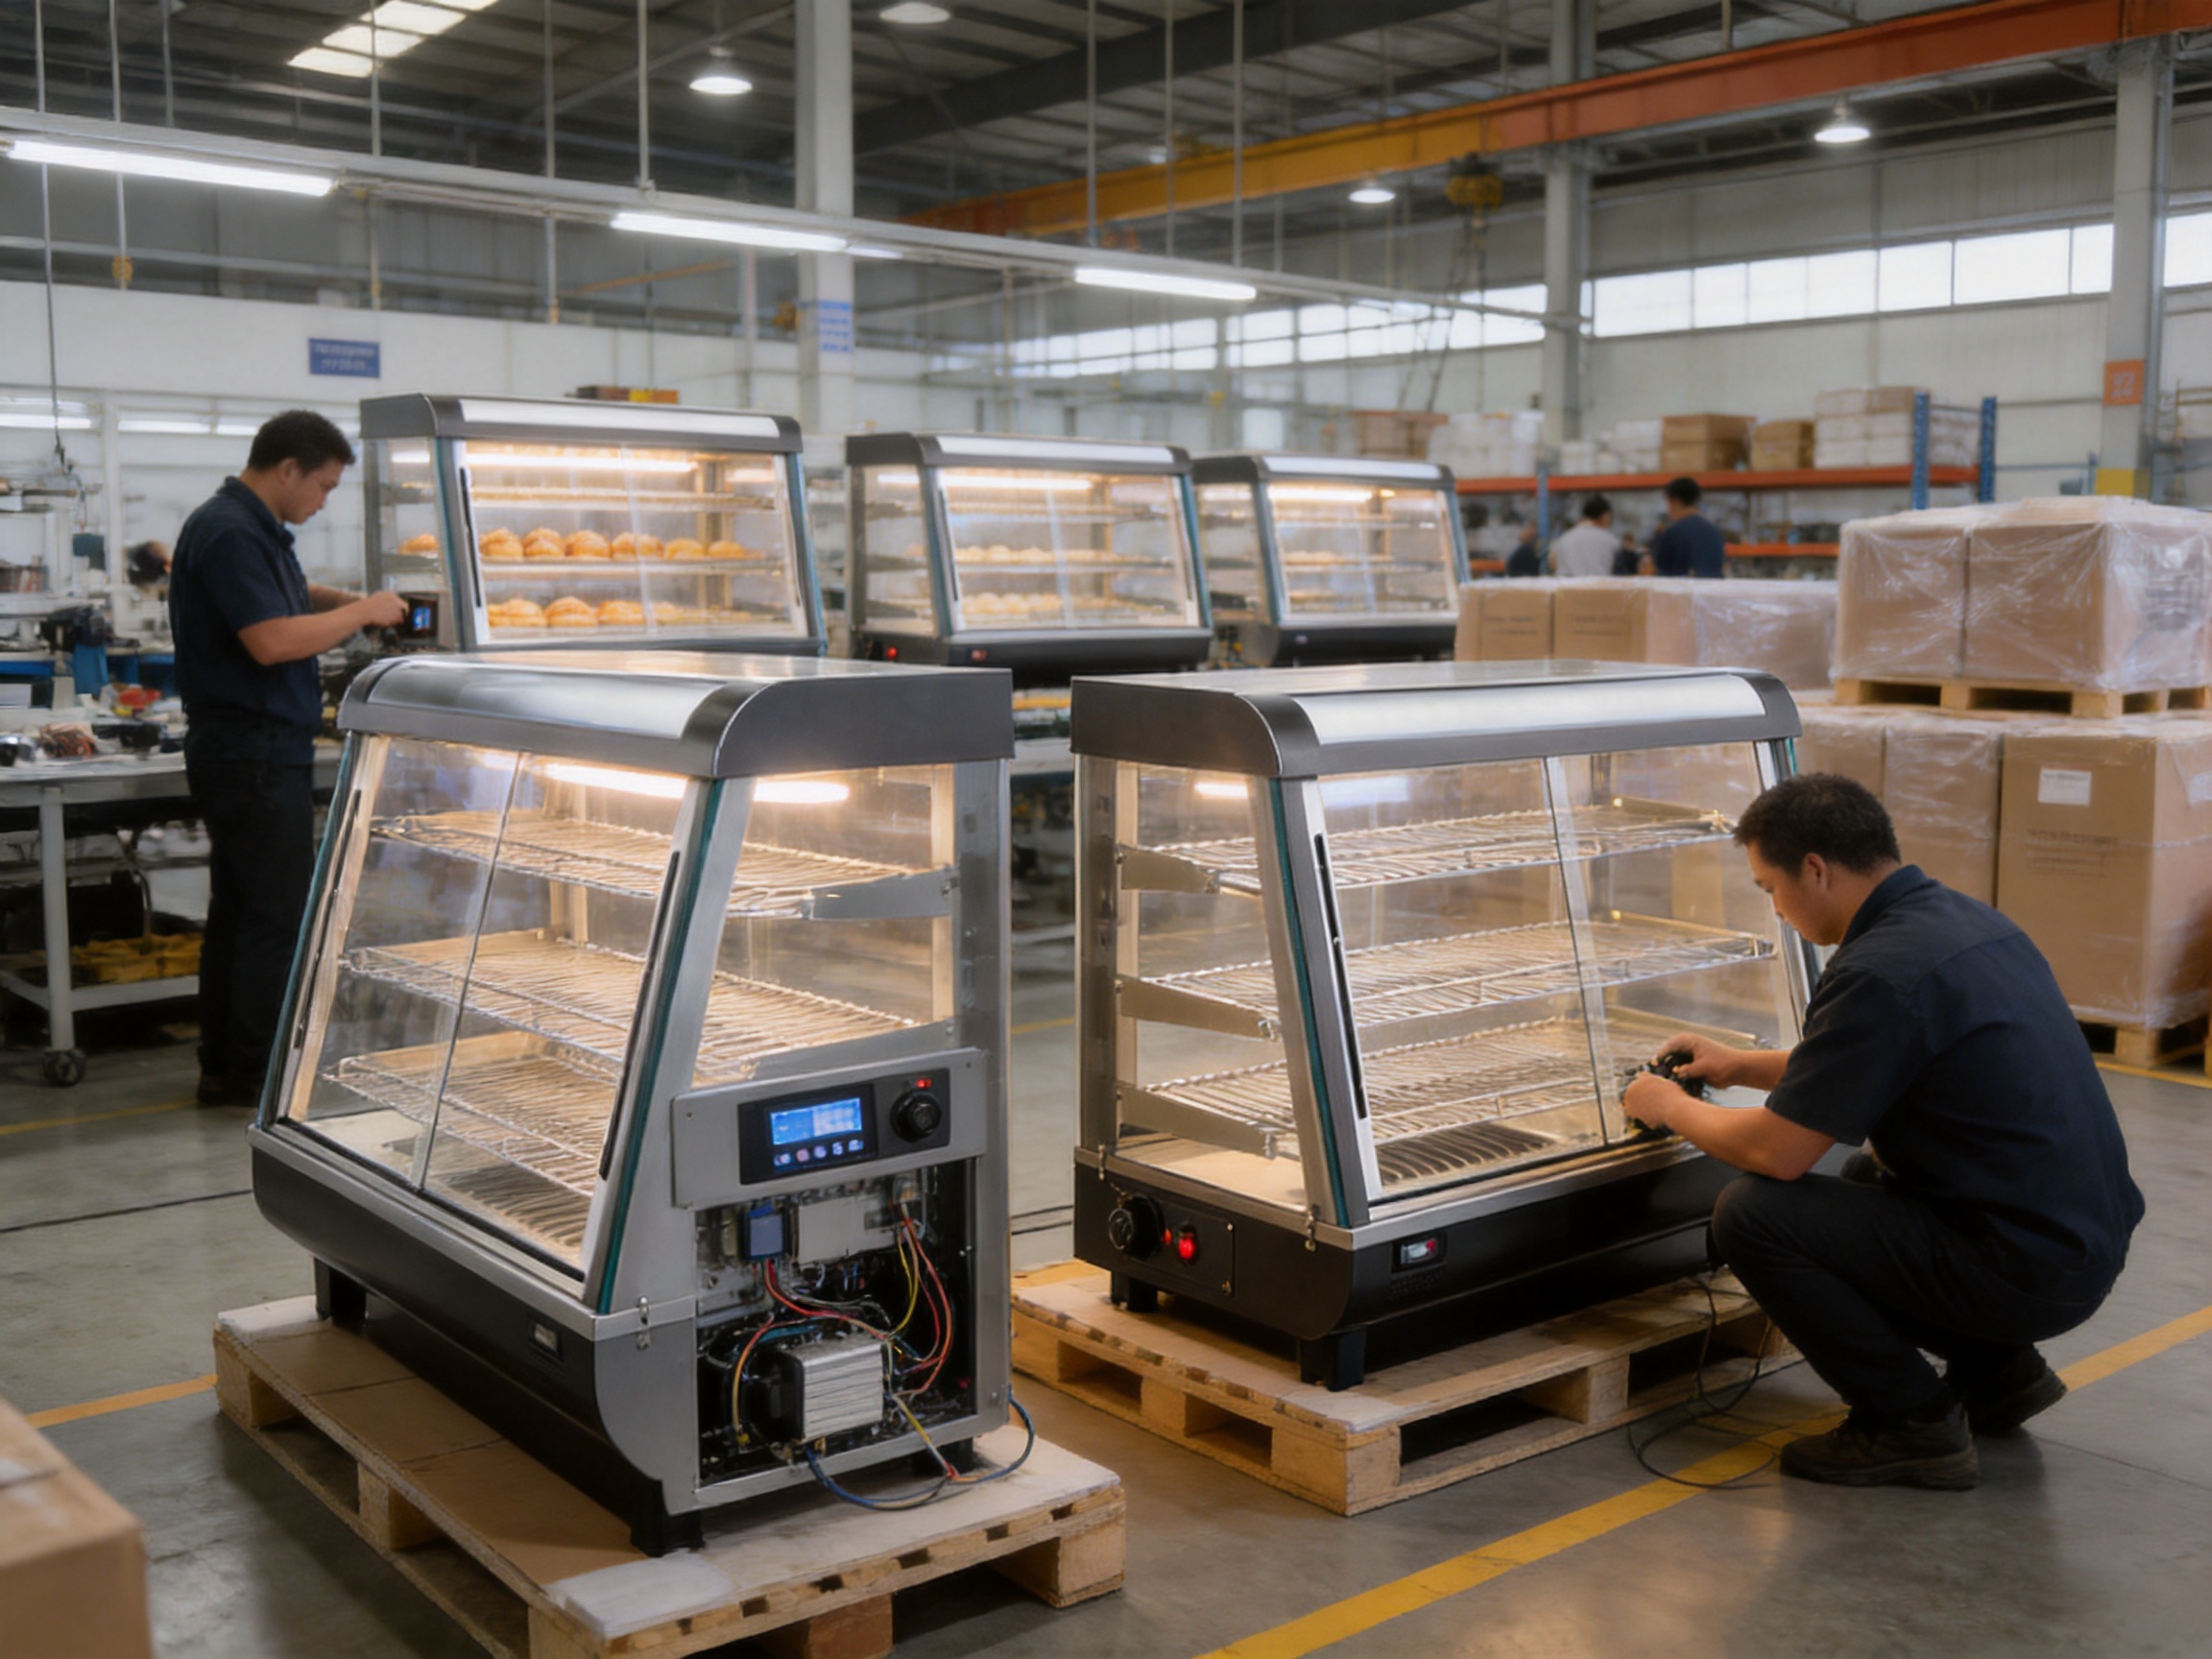
The manufacturer behind the product was established in 2007 and has more than ten years of experience in the development and production of vertical display cabinets, cake cabinets, warming cabinets, and related commercial refrigeration equipment. This experience is relevant because commercial display equipment requires coordination between thermal systems, cabinet construction, electrical controls, lighting, moisture management, packaging, and quality inspection.
The company operates a modern management garden factory covering approximately 40,000 square meters. A facility of this scale can support organized production planning, dedicated work areas, inventory control, assembly operations, product testing, and coordinated quality procedures. The size of a factory alone does not guarantee product performance, but it can provide a stronger foundation for repeatable manufacturing than a small workshop with limited process control.
The company also maintains a professional research and development team. Product development in this sector involves more than changing external appearance. Engineers must consider temperature stability, component compatibility, energy use, structural strength, service access, drainage, lighting, insulation, control interfaces, and shipping protection. A dedicated research and development capability supports continuous improvement in these areas.
Advanced testing facilities are identified as part of the company’s manufacturing resources. Testing is important for commercial equipment because a unit may face long operating hours, frequent loading changes, repeated door or access cycles, varying ambient temperatures, transport vibration, and demanding cleaning routines. Product testing can help identify weaknesses before equipment reaches the customer.
The manufacturer states that it has obtained CE, GS, CCC, CB, RoHS, ETL, and other major certifications. Certification requirements vary by market and product configuration, and buyers should confirm the exact certification coverage for the model and destination country. Nevertheless, the presence of internationally recognized certification experience indicates familiarity with formal product safety, electrical, material, and compliance requirements.
RoHS-related compliance is relevant to material and restricted-substance considerations. Electrical and safety certifications can help importers and distributors evaluate whether a product is suitable for their target market. Buyers should request current documentation, test reports, declarations, and applicable certification files as part of the procurement process.
10. Quality Control from Component Selection to Shipment
A reliable commercial display warmer depends on the quality of many individual elements. These may include the thermostat, display, evaporator components, lighting assembly, wiring, cabinet panels, insulation, glass, seals, fasteners, drainage components, and packaging materials. A weakness in any one area can affect the customer’s operating experience.
Manufacturing quality begins with appropriate component selection. Suppliers need to consider compatibility, expected operating conditions, availability of replacement parts, and consistency between production batches. Standardized components can simplify assembly and service, while carefully selected specialized parts can support product performance in demanding applications.
Assembly quality is equally important. Electrical wiring should be organized and protected. Control components should be installed consistently. Internal channels should be fitted correctly. Glass panels and cabinet structures should be aligned to support appearance and safe operation. A well-defined assembly process helps reduce variation from one unit to another.
Functional testing should verify that the equipment powers on correctly, responds to control inputs, illuminates the display area, and operates within the intended product parameters. Testing procedures may also examine thermal behavior, defrost operation, drainage, electrical safety, and abnormal conditions. The specific tests used should be confirmed with the supplier during technical discussions.
Packaging is an important part of manufacturing quality because commercial cabinets may travel long distances before installation. The XCR-136L has a gross weight of 41 kilograms and package dimensions of 963 by 549 by 675 millimeters. Proper packaging must protect the cabinet from impact, vibration, surface damage, and handling stress. Distributors should inspect shipments upon arrival and document any damage promptly.
The stated container quantities are 72 units in a 20-foot general-purpose container and 192 units in a 40-foot high-cube container. These figures can assist importers with preliminary logistics planning. Actual loading should be confirmed with the supplier because packaging revisions, shipping regulations, pallet requirements, and container-loading methods may affect final quantities.
11. Installation and Operating Considerations
Correct installation is essential for the best possible performance. The cabinet should be placed on a stable, level counter capable of supporting its weight and the weight of the displayed products. Uneven placement may affect alignment, drainage, access, and the overall appearance of the showcase.
The installation site should provide suitable electrical service for the 1100-watt input requirement. Buyers should confirm voltage, frequency, plug type, circuit protection, and local electrical regulations before purchase. A qualified installer or authorized service professional should be used where local requirements call for one.
Around the equipment, staff should maintain adequate clearance for ventilation, cleaning, inspection, and service. The cabinet should not be pressed against heat-producing appliances, exposed to direct sources of excessive heat, or installed where airflow is obstructed. The supplier’s installation instructions should take precedence over general guidance.
Before loading food, staff should clean the accessible internal surfaces and confirm that the controls, light, and display operate correctly. The unit should be allowed to reach the desired operating condition before products are placed inside. Loading should not block internal airflow paths, water channels, lights, or service areas.
Products should be arranged so that customers can see them easily and staff can rotate stock according to the business’s established procedures. Overloading can reduce the effective performance of any display warmer. It can also make products difficult to remove, increase the chance of spills, and obstruct visibility.
12. Cleaning, Hygiene, and Routine Maintenance
A display warmer is part of the food service environment, so hygiene must be treated as a daily operating priority. Staff should establish a cleaning schedule covering the glass, interior surfaces, trays or shelves, water channel, control area, exterior panels, and accessible seals. Cleaning products should be compatible with the materials and should be used according to the equipment instructions.
Food residue should not be allowed to accumulate in corners, joints, or drainage areas. The water channel beneath the top evaporator deserves particular attention because blockage or residue may interfere with moisture management. It should be inspected at regular intervals and cleaned using an appropriate method.
The LED light and digital display should be kept clear enough for staff and customers to see them. Glass should be cleaned with a suitable non-abrasive product to reduce streaking and prevent surface damage. Abrasive pads, aggressive chemicals, and excessive water around electrical controls should be avoided unless expressly approved by the manufacturer.
Operators should monitor unusual noise, unexpected temperature changes, damaged seals, flickering lights, water accumulation, or control errors. Early reporting can prevent a minor issue from becoming a larger service problem. Businesses with multiple units should maintain a simple equipment log that records cleaning, inspection, temperature checks, and service actions.
13. Energy and Operational Efficiency
The rated input power of the XCR-136L is 1100 watts. This figure identifies the input power specification, but actual energy consumption depends on operating time, ambient temperature, product loading, control settings, defrost cycles, installation conditions, and usage frequency. Buyers should avoid estimating operating cost from rated input alone.
Efficient operation begins with correct loading and sensible temperature selection. Setting the cabinet higher than necessary may increase the thermal burden and affect product quality. Leaving the access area open for extended periods can also increase the workload on the system. Staff should organize products in advance so that replenishment is quick and controlled.
Cleaning and maintenance can support efficiency by keeping heat-transfer and drainage components in suitable condition. Blocked channels, dirty surfaces, damaged seals, or obstructed ventilation can cause the equipment to work harder. A routine maintenance program can therefore support both performance and operating cost control.
LED illumination is another practical efficiency feature. It provides internal product visibility while generally producing less unwanted heat than older lighting formats. The lighting should still be switched and maintained according to the operating instructions and the business’s display schedule.
14. Choosing the Right Display Warmer for a Business
Before purchasing, operators should define the products that will be displayed, the required holding temperature, the expected turnover, the available counter space, and the likely service hours. A warmer for delicate pastries may have different requirements from a warmer used for prepared savory foods. Menu planning should therefore come before equipment selection.
Capacity should be assessed in relation to sales volume rather than selected only by the largest available number. A 136-liter cabinet can be advantageous when the business wants a focused, frequently refreshed display. Smaller batches may look more appealing and may reduce the time food spends in the cabinet before sale.
Visibility is another important criterion. Customers should be able to see the products from the normal approach angle. The cabinet should not be hidden behind menus, point-of-sale equipment, or other counter objects. The internal LED light can support visibility, but overall placement remains the responsibility of the operator.
Purchasers should also evaluate after-sales support, spare parts, documentation, warranty coverage, certification, shipping terms, and local service capability. A good product specification is only one part of a successful commercial equipment investment. The supplier’s ability to communicate clearly and support international buyers can be equally important.
15. Why Manufacturing Experience Matters to Buyers
Commercial equipment buyers often compare products that appear similar from the outside. Two display warmers may have comparable dimensions, but their internal construction, control reliability, testing standards, and manufacturing consistency may be different. This is why the supplier’s background matters.
More than a decade of sector experience can help a manufacturer understand recurring customer requirements. These may include easier cleaning, better display visibility, simpler controls, reliable packaging, stable component sourcing, and compatibility with international market requirements. Experience does not replace product verification, but it can improve the supplier’s ability to identify and address practical problems.
A dedicated research and development team can also make it easier to adapt products for different markets. Buyers may require different electrical configurations, labeling, packaging, documentation, or certification packages. These requirements should be discussed before production rather than treated as last-minute changes.
A factory with organized production lines and testing facilities can support larger wholesale programs. This is relevant for distributors, importers, chain stores, and hospitality groups that need consistent products across multiple orders. The stated container-loading capacity also indicates that the model is suitable for planned commercial distribution rather than only individual retail purchase.
16. Wholesale and Distribution Potential
The XCR-136L is suitable for wholesalers and distributors seeking a compact display warmer for bakery, café, convenience, restaurant, and hotel customers. Its application range allows distributors to present it to multiple market segments instead of relying on one narrow use case.
For wholesale planning, the 20-foot and 40-foot container quantities provide an initial basis for logistics estimates. Distributors should calculate the complete landed cost, including product price, freight, insurance, duties, local delivery, storage, handling, installation, and after-sales service. Packaging dimensions should also be considered when planning warehouse space.
Product training can improve distributor performance. Sales staff should understand the temperature range, input power, capacity, dimensions, standard features, installation requirements, and intended applications. They should also communicate that food safety depends on correct procedures, product-specific requirements, and local regulations rather than on the display cabinet alone.
Distributors may benefit from offering complementary equipment, such as refrigerated cake showcases, vertical display coolers, countertop display refrigerators, sushi showcases, open display coolers, and four-sided glass freezers. A broader equipment range can help customers develop a coordinated front-of-house layout.
17. Frequently Asked Questions
Q1: What is the capacity of the XCR-136L?
The rated capacity is 136 liters. The usable arrangement will depend on the internal layout, the size of trays or containers, and the need to maintain suitable airflow and product visibility.
Q2: What temperature range does the display warmer provide?
The stated temperature range is 30°C to 90°C. Operators should select a setting based on the food type, holding period, internal procedures, and applicable food-safety requirements.
Q3: Is the cabinet suitable for cakes?
The product is described as a food display warmer and cake showcase. It may be suitable for selected cake or bakery applications, but users should confirm whether the intended product requires warming, cooling, or ambient display before installation. Chilled cakes should generally be placed in equipment designed for refrigerated storage.
Q4: What type of control does the unit use?
The XCR-136L includes a digital thermostat and display. This allows staff to view and manage the selected temperature more clearly than with a basic mechanical control.
Q5: Does the product include lighting?
Yes. The standard features include an internal top LED light intended to improve the visibility and presentation of displayed products.
Q6: What is the purpose of the top and bottom evaporators?
The top and bottom evaporator arrangement is designed to support the internal thermal environment across the display area. Actual results depend on loading, ambient conditions, product placement, installation, and maintenance.
Q7: Does the display warmer have automatic defrost?
Yes. Automatic defrost is listed as one of the standard features. Routine cleaning and inspection are still required, especially around moisture-management areas.
Q8: What is the input power?
The rated input power is 1100 watts. Electrical voltage, frequency, plug configuration, and circuit requirements should be confirmed for the destination market before ordering.
Q9: How large is the unit?
The product size is 904 by 486 by 636 millimeters. The package size is 963 by 549 by 675 millimeters. Buyers should allow additional space for installation, ventilation, service, and access.
Q10: How much does the product weigh?
The net weight is 38 kilograms and the gross weight is 41 kilograms. The gross figure includes packaging and should be used when planning transport and handling.
Q11: Is it suitable for a small café?
Its compact counter-oriented dimensions and 136-liter capacity can make it suitable for a small café, especially when the business needs a focused display of warm products. The final decision should consider menu volume, counter strength, electrical service, and customer flow.
Q12: Can it replace a refrigerator?
No. The XCR-136L is a display warmer, not a general-purpose refrigerator. Products that require chilled storage should be displayed in suitable refrigerated equipment.
Q13: What maintenance does the unit require?
Routine care should include cleaning internal and external surfaces, inspecting the water channel, keeping the glass clear, checking the display and LED light, monitoring temperature performance, and reporting unusual operating conditions. The manufacturer’s instructions should be followed for detailed service procedures.
Q14: What certifications are associated with the manufacturer?
The manufacturer states that it has obtained CE, GS, CCC, CB, RoHS, ETL, and other major certifications. Buyers should request current documents and confirm that the specific model and configuration meet the requirements of the destination market.
Q15: Is the model available for wholesale orders?
The stated container quantities are 72 units in a 20-foot general-purpose container and 192 units in a 40-foot high-cube container, indicating suitability for commercial distribution. Final quantities should be confirmed with the supplier based on packaging and loading arrangements.
18. Final Assessment
The XCR-136L is a practical commercial display warmer for businesses that need controlled warming and attractive product presentation in a compact counter format. Its 136-liter capacity, 30°C to 90°C temperature range, 1100-watt input specification, digital thermostat, internal LED lighting, dual evaporator arrangement, water channel, direct cooling system, and automatic defrost provide a coordinated set of features for professional food service.
Compared with basic heated shelves or manually controlled display solutions, the model offers greater control, more organized moisture management, improved product visibility, and a more complete commercial equipment design. Its dimensions make it suitable for cafés, bakeries, restaurants, hotels, convenience stores, takeaway counters, and other businesses where counter space and customer presentation are important.
The manufacturer’s experience since 2007, approximately 40,000-square-meter factory, professional research and development team, testing facilities, and stated international certification experience provide additional reasons for distributors and commercial buyers to examine the product. These capabilities support a manufacturing approach focused on product development, testing, repeatability, and international market requirements.
Successful use still depends on correct installation, appropriate temperature selection, sensible loading, cleaning, staff training, and compliance with local food-handling rules. When these practices are combined with the cabinet’s built-in features, the XCR-136L can help businesses create a cleaner, more visible, and more controlled warm-food display.
References
1. Product specification sheet for the XCR-136L commercial food display warmer.
2. Manufacturer-provided standard feature information for commercial warming and display equipment.
3. General principles of commercial food holding, temperature control, and hygienic equipment operation.
4. General guidance on commercial refrigeration, food display equipment, and retail merchandising design.
5. General principles of electrical product conformity, restricted substances, and international equipment certification.
6. Commercial equipment installation, cleaning, preventive maintenance, and safe operating practice references.
Product: Display Equipment Food Display Warmer Cake Showcase
You May Also Like
-
- Navigation
- Home
- About Us
- Products
- News
- Contact Us
 East Zone, Guanhaiwei Industrial Park, Cixi City, Ningbo, Zhejiang, China
 +86-574-63668678
 +86-574-63668108

Copyright © Ningbo XiangChi Electrical Co.,Ltd All Rights Reserved.